About MedIntegrity LLC
We make the instruments that tell you a filter held, a glove is intact, a vial is sealed, and your water is clean. That's the whole business. We've been at it for 15 years.
Who we are
MedIntegrity LLC is a U.S.-based manufacturer and supplier of precision testing instruments and related consumables for the pharmaceutical and biotechnology industries. We focus on technologies that support product quality, process control, contamination prevention and reliable testing in regulated manufacturing and laboratory environments.
Our equipment sits on the production floor and in the QC lab, where it has to be right every single run — not most runs. Filter integrity testers. TOC analyzers. Glove integrity testers. Container-closure and packaging leak systems. Freezing-point osmometers. And the cartridge filters, filter housings and accessories that go with them.
The common thread is simple: a measurable answer you can stand behind in front of an auditor. If a test can't be documented, it's not really a test.
We work with customers to identify the equipment and testing solutions suited to their applications, technical requirements and operating environments — then we size the configuration rather than making the application fit a standard one.
Our Partners
Fifteen years of supply into pharmaceutical, biotech and water-treatment operations worldwide. These are some of the brands behind the 500+ cooperative customers on our reference list.
Names on this wall are reference relationships MedIntegrity can put on a call. Ask us for the references that match your application and region — we would rather you check than take the wall on faith.
By the numbers
Inside Our Factory
Our instruments are built at our own manufacturing base — 600 acres of production floor, warehouse and test benches, with an annual output of roughly 2,000 units.
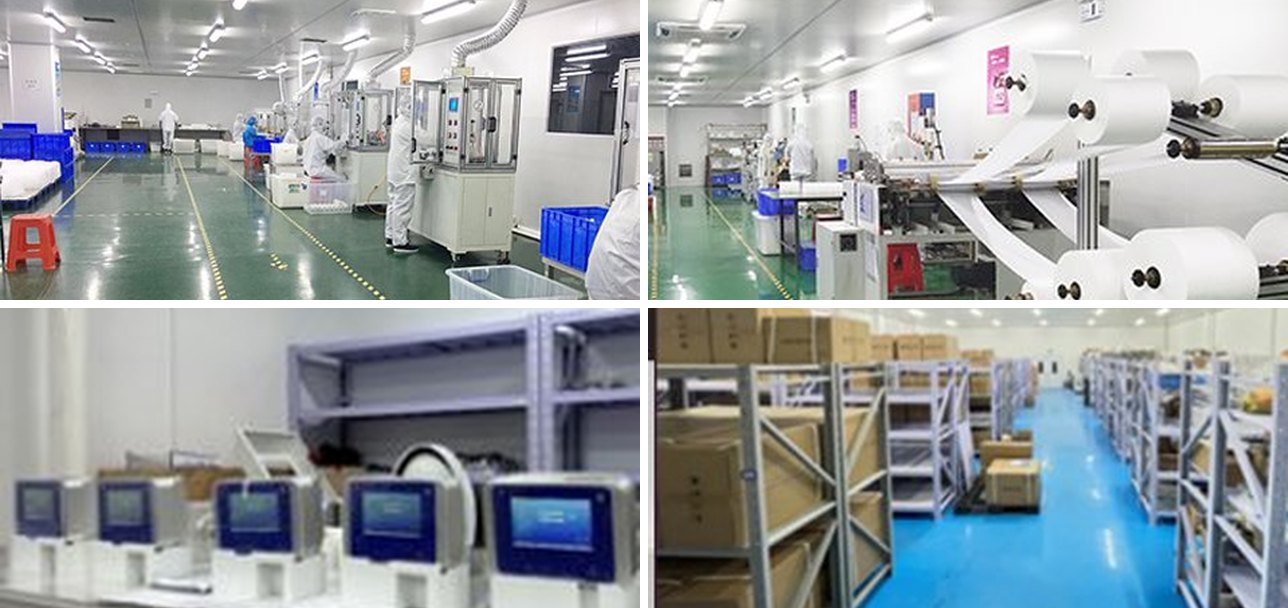
Assembly runs from electronics and pneumatic manifolds on the bench line through final commissioning in the clean assembly rooms, with the finished-goods warehouse holding instrument stock and spares for every model we ship. That is what makes "built in our own factory" more than a phrase on a spec sheet: the line that builds your instrument is the line that supports it.
Because we control the build, configuration is negotiable. Ports, filter-size ranges, accessories, software record formats — the conversations our engineers have with you before the order are the same people who will assemble and commission the unit.
Tour It on a CallQualifications & Standards
What our instruments are built and tested against — and the documentation that comes with them.
Regulatory alignment
Testing methods satisfy FDA and GMP requirements as well as USP and EP — the standards your audit will measure the result against, not a marketing badge.
Compendial methods
USP <43> / EP 11.0 filter integrity, USP <1207> container-closure integrity, ASTM F2338 vacuum decay, and the TOC and osmolality methods behind pharmaceutical water testing.
Data integrity
21 CFR Part 11 support with electronic records and audit trails sized for five years or more; development follows GAMP guidelines.
Qualification package
Every instrument ships with IQ/OQ/PQ documentation guides — validation arrives with the instrument instead of becoming a project a year later.
Patents
28 patented products across the portfolio — the design decisions inside the instruments, on record.
On request
Certificates, conformity documents and full specification sheets are available on request — the fastest route is a note to your MedIntegrity representative.
Who runs our equipment
BeiGene USA operates 20 WGT-1200 glove integrity units. Sunny Pharmaceutical in Egypt runs the WGT-1000 Online on routine aseptic-line checks. They're among the referenced customers we point to — and the reason we take the spec sheets seriously.
How we work
A short list. We mean every word of it.
Working principle
Seek truth from facts. Tell the truth. Do practical things. In an audit-heavy industry, the instrument, the document and the promise all have to say the same thing.
What we stand behind
A conscience enterprise that is also a reliable one — real specifications, no borrowed claims. If a number is on our site, someone can defend it.
Business philosophy
Innovation and development, integrity wins the world. Twenty-eight patented products, built the same way for fifteen years.
Service is part of the instrument
We don't hand you a box and disappear. Product selection, consultation, installation coordination, training, troubleshooting, after-sales — the whole life of the instrument. When something's off at 2 a.m. on a production night, you want someone who knows the machine to answer the phone. That's us.
Why pharma manufacturers keep our instruments on the line
The common denominator across 500+ customers is not the spec sheet — it is the record. Every MedIntegrity instrument is built to produce a result in a form the quality system can hold: an electronic record with method, parameters, result, operator and time; an audit trail sized for five years or more; and a qualification documentation package (IQ/OQ/PQ) that brings the instrument inside your validated environment from day one.
Development follows GAMP guidelines with 21 CFR Part 11 support, and the methods are aligned to FDA and GMP requirements plus USP and EP. The result is that validation is not a project you start after the instrument arrives — it is a document set that arrives with it. That is the difference between an instrument you can defend at audit and one you have to rebuild your story around.
What the numbers mean
15 years focused on pharmaceutical testing equipment. 28 patented products. A 600-acre manufacturing base turning out roughly 2,000 instruments a year. 500+ customers served — and referenced customers you can ask about: BeiGene USA operating 20 WGT-1200 glove integrity units, Sunny Pharmaceutical in Egypt running the WGT-1000 Online for routine aseptic-line inspection. We take the spec sheets seriously because someone, somewhere, is reading them in an audit.
Frequently Asked Questions
Where is MedIntegrity based?
MedIntegrity LLC is U.S.-based in Santa Clarita, California, with a U.S. service team that handles installation coordination, training, troubleshooting and after-sales across time zones.
Where are MedIntegrity instruments manufactured?
In our own manufacturing base — 600 acres of production, assembly and warehousing with an annual output of roughly 2,000 units. We are the manufacturer, not a reseller: configuration conversations, commissioning and spares all run through the team that built the instrument.
Which standards do your instruments support?
Testing methods aligned with FDA and GMP requirements, plus USP and EP — including USP <43> for filter integrity, USP <1207> for container-closure integrity, and the TOC and osmolality methods behind pharmaceutical water and product testing. Development follows GAMP guidelines with 21 CFR Part 11 support.
Can you provide certificates and reference customers?
Yes. Certificates, conformity documents and full specification sheets are available on request, and we will put reference customers from your application and region on a call — including names from our partner wall such as BeiGene USA.
How many instruments do you offer?
19 instrument models across seven product lines: filter integrity testers, glove integrity testers, container-closure integrity systems, packaging leak testers, RTP integrity testers, TOC analyzers and a freezing-point osmometer.
Need a quote or technical advice?
Tell us your application — our U.S. team responds with product selection, documentation and pricing.
Request a Quote